
Compare molded pulp inserts in the stacks you will receive, as well as in the finished gift box. Record the height of a known number of empty inserts and observe whether one part separates cleanly. A compact stack is useful only if its supplied arrangement also suits your storage and packing work.
Establish how the empty inserts will arrive
An insert can look suitable beneath a candle jar while leaving a different buying question unanswered: what happens before the jar goes in? The packer needs to receive the empty parts, put them within reach and take one for each gift. A photograph of one insert cannot show that sequence.
Nesting means that parts sit partly inside one another. Their actual stack height depends on how those particular parts meet. MFT-CKF’s molded fiber manufacturing overview describes designing its products for nesting and pallet loading. That identifies a design consideration, rather than establishing a saving for an unspecified supplier’s insert.
Identify the proposed component, revision and supplied orientation. Ask whether the delivery contains nested stacks, loosely stacked parts or another arrangement. A delivery carton may hold several stacks with separators or wrapping; its outside dimensions and usable count remain separate facts.
If you are still choosing the complete construction, first compare one-piece trays and separate end supports. The check here starts with one selected empty component. It does not combine left and right supports into an unexplained stack count.

Measure the stack you actually intend to store
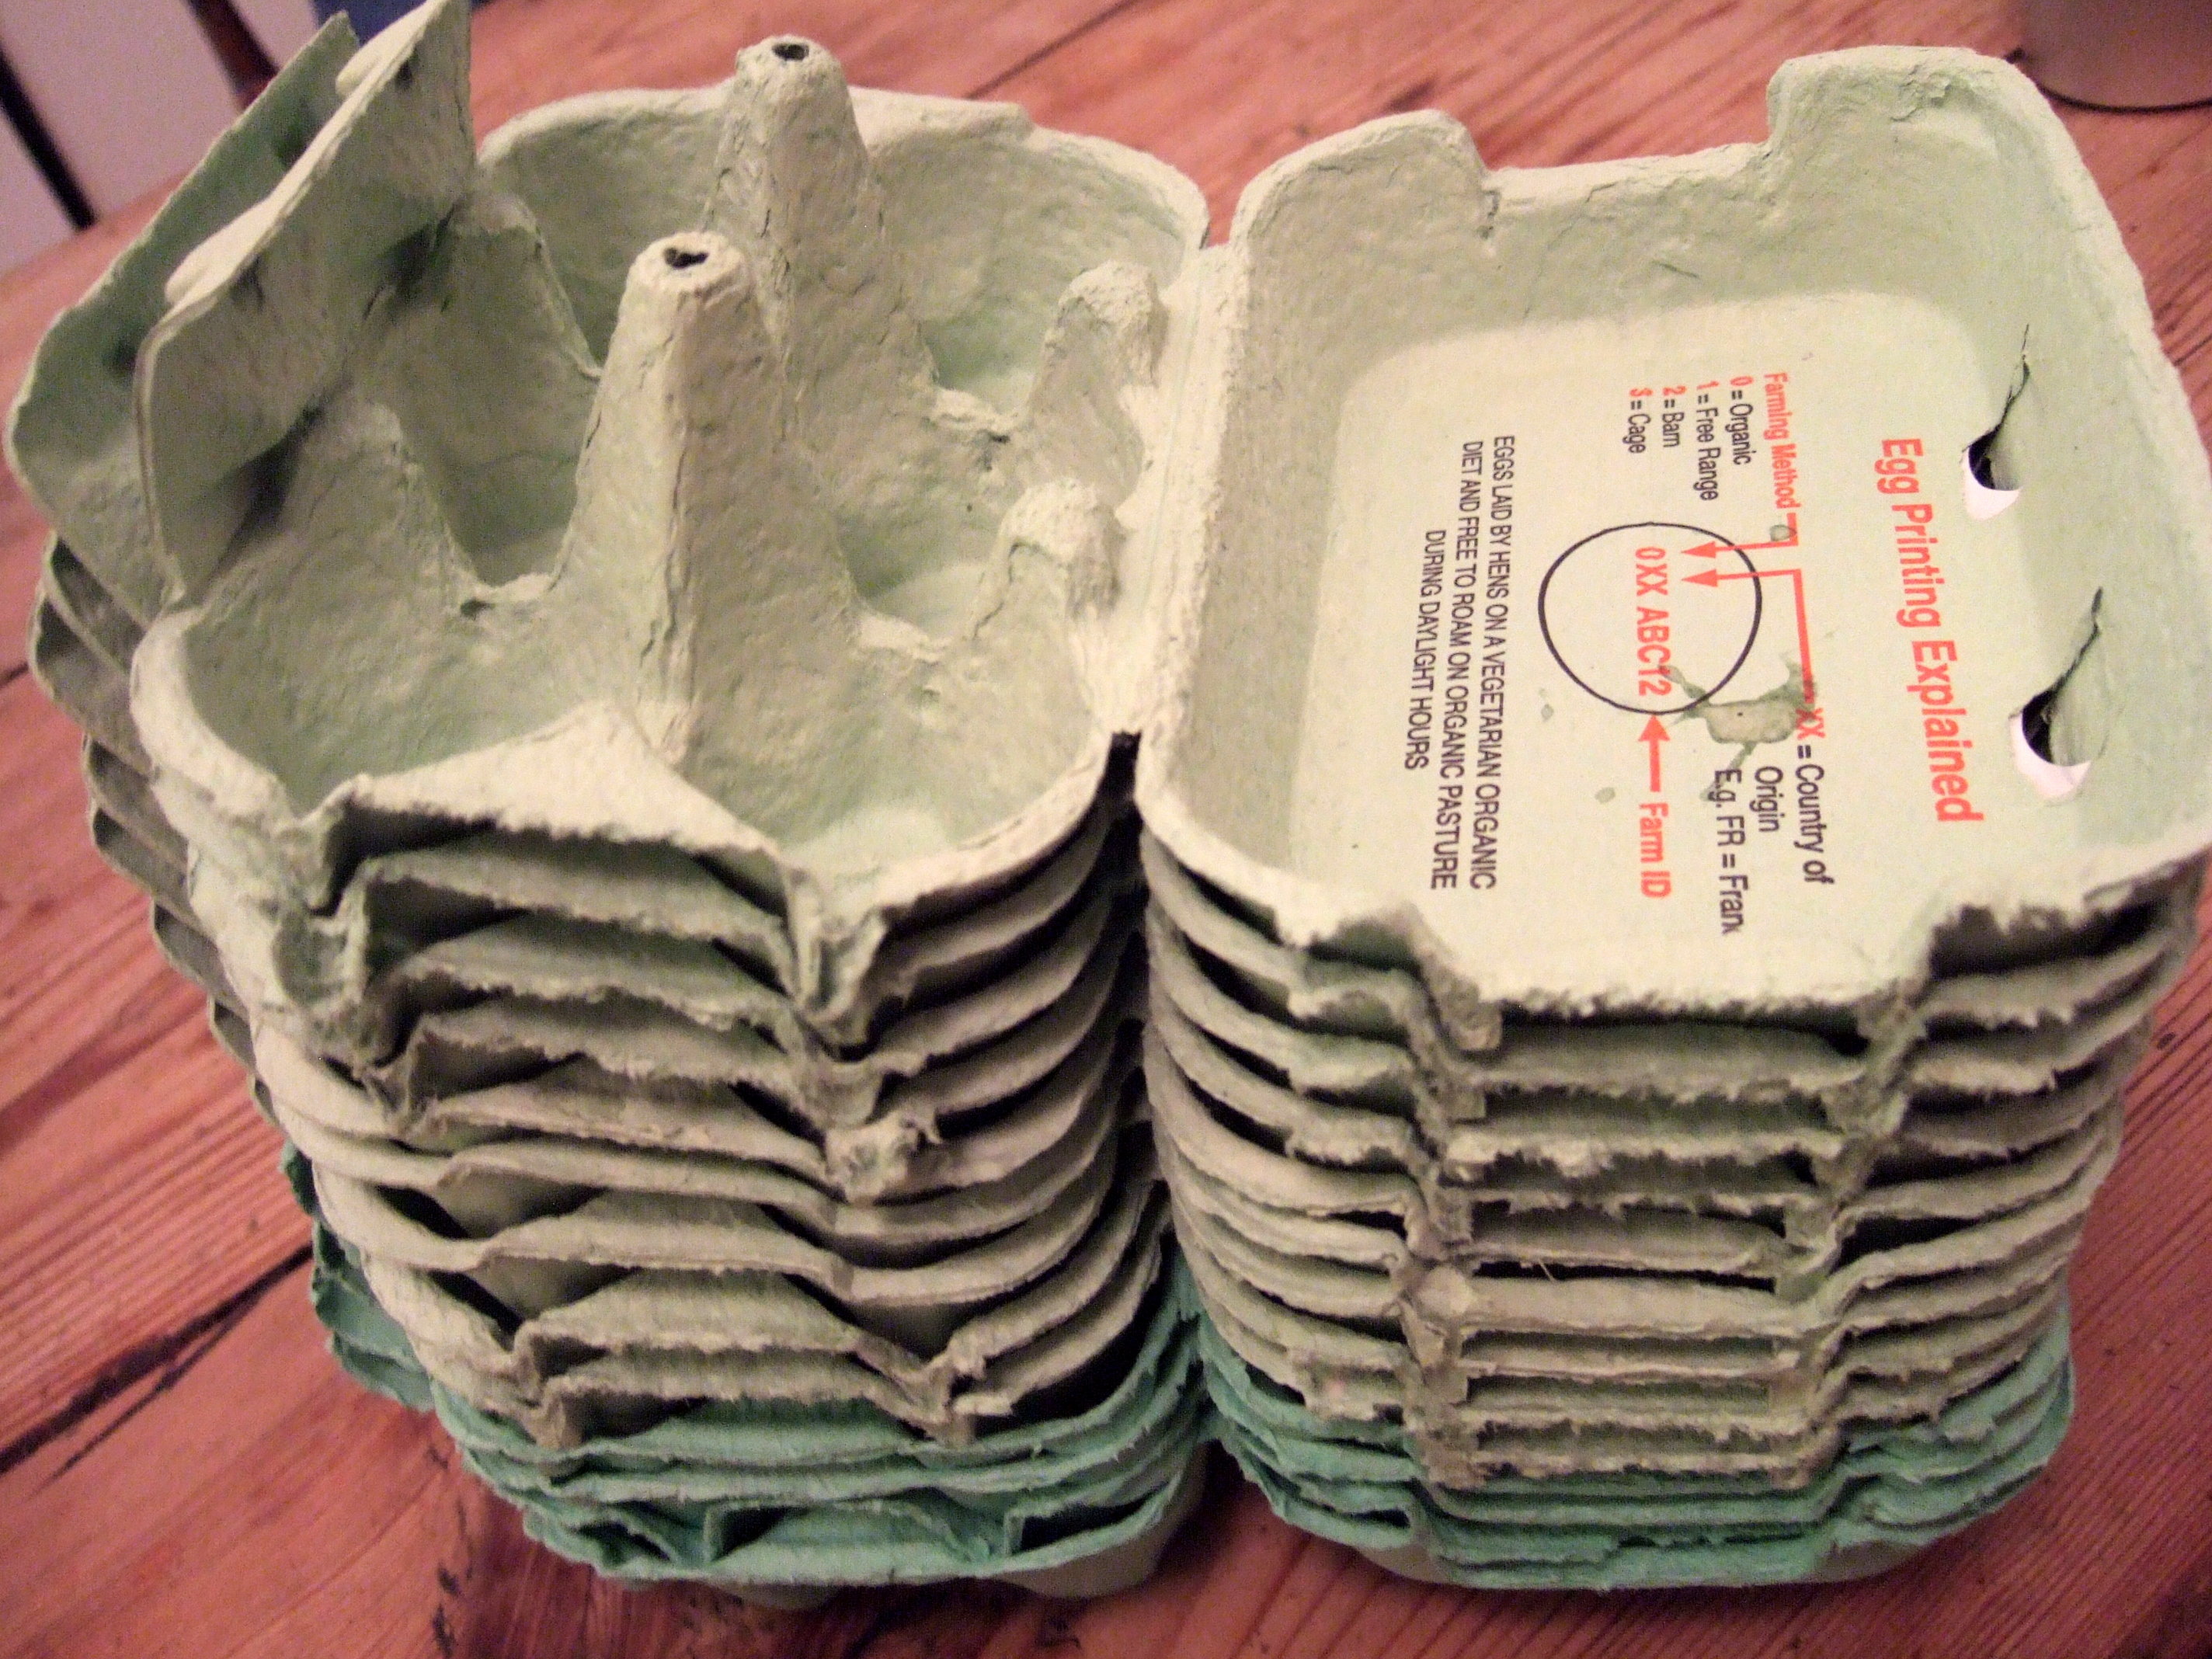
Keep three measurements apart: one empty part’s height, the height of a counted stack, and the outside size of its delivery carton. Multiplying the first by the part count describes an unnested column. It cannot establish the height of a nested stack.
Count the actual parts used for the stack measurement. Record their orientation, the supporting surface and whether wrapping or compression remains. A stack measured after loosening a tight shipping bundle is a different state from that bundle on arrival. Preserve both descriptions if they matter to your receiving work.
A supplier can provide a photograph beside a scale, with the stack count and component reference visible. Ask for the carton contents as well: stacks per carton, pieces per stack and any separate loose parts. This lets you reconcile a quoted piece quantity with the containers that will reach your premises.
The carton information determines whether the stack fits the proposed storage space. Access also matters. A stack that occupies a shelf but cannot be reached for normal picking has not answered the packing requirement. Compare the supplied arrangement with the space you actually have, rather than turning a stack-height difference into a freight saving.
Observe whether one pick gives you one usable part
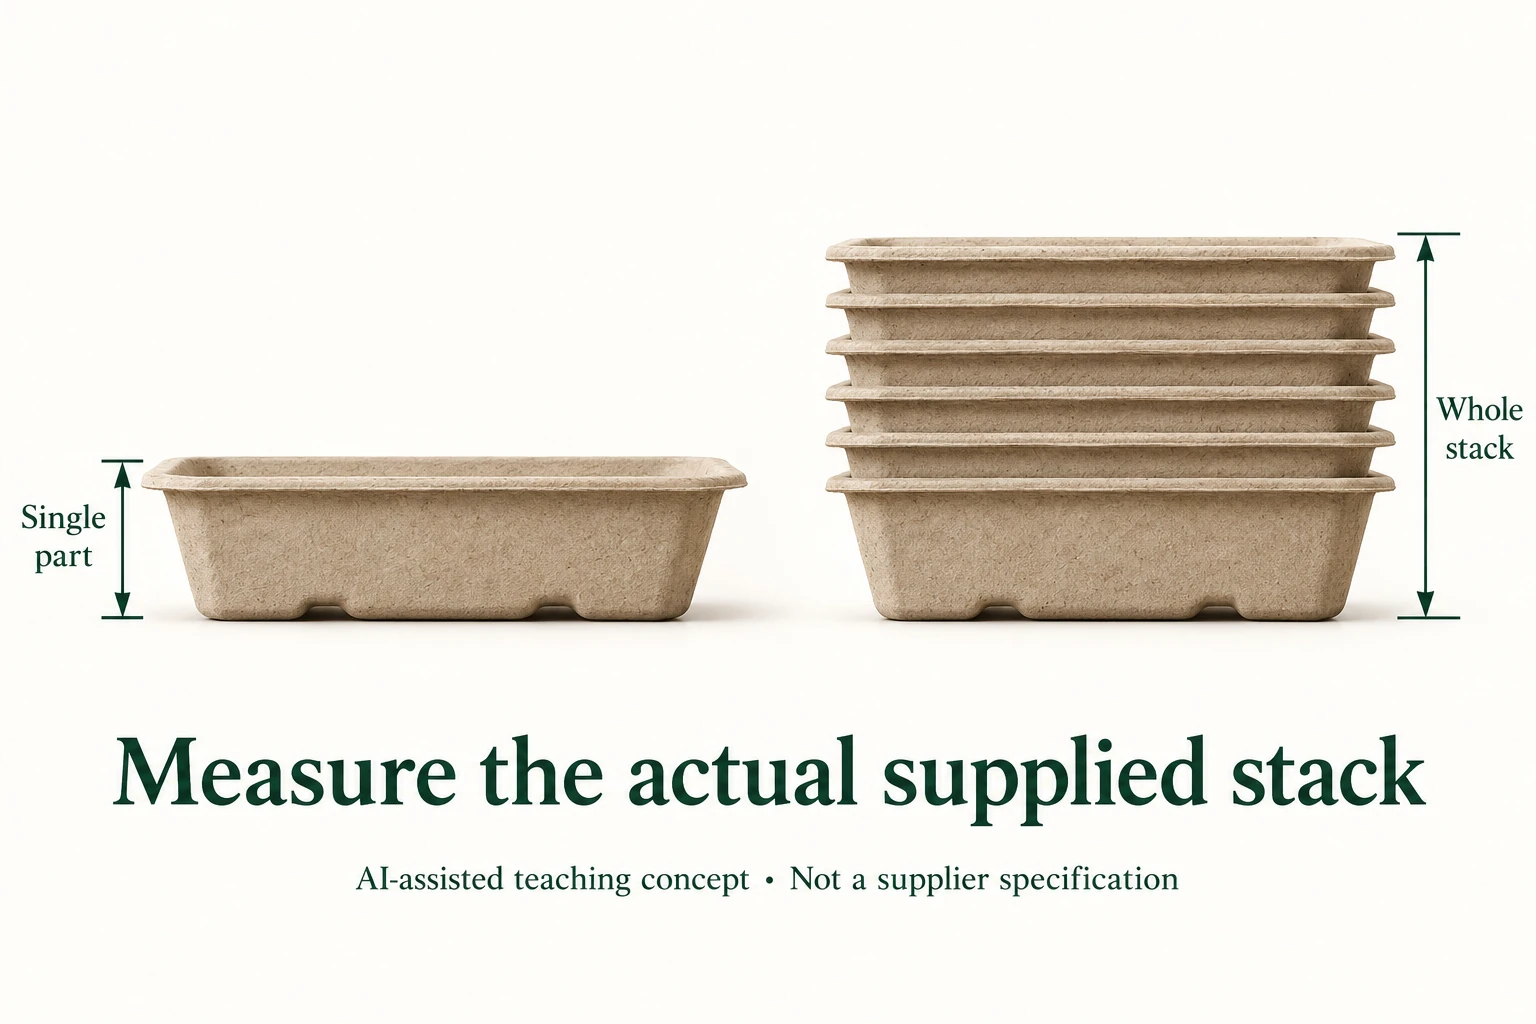
Try the empty stack in the position intended for packing. Use the ordinary proposed hand action and note what leaves the stack. One part, two attached parts and a part with a damaged edge create different next steps. Keep the original supplied state visible before separating or rearranging everything for the demonstration.
Wynalda Packaging’s design article dated June 30, 2026 explains that trays can nest too tightly and discusses de-nesting posts. Those features are a possible supplier design response. They are not instructions to add an arbitrary spacer, change the tool yourself or assume the revised insert will behave as intended.
When two parts come away together, show the pair before pulling them apart. Record where they meet and whether ordinary handling separates them. If the operator changes grip, twists the stack or uses another object, retain that action in the observation. A successful pick after rearranging the stack does not describe the original action.
Continue to note where in the stack a difficulty appears. An easy first pick leaves the remaining parts unobserved. Keep the carton, bundle and component references with the record so a later reply can address the same material. If the demonstration uses a different prototype or unpacked sample, state that difference before applying its result to the proposed delivery.
PiP Automation describes tray denesting as separating nested trays individually and emphasizes testing actual production packaging. Its equipment guidance supports the distinction between nesting and separation. It does not establish a need for a small brand to buy a machine.
This empty-part check is separate from removing a product from its pulp cavity. Easy separation of empty trays says nothing about how a customer removes the packed candle.
Compare two hypothetical deliveries for the same candle pack
Suppose a fictional candle brand is considering 500 empty inserts. Two proposals target the same jar-and-box requirement, but their finished fit remains unreviewed. For this exercise only, both use 50 parts per stack. Assume C’s stack is 24 cm high and D’s is 31 cm high. These are invented planning inputs, not supplier measurements.
The comparison deliberately leaves separation and carton information open. A buyer can replace the exercise entries with actual identified proposals and add observations before deciding.
Scroll this comparison table to see all columns.
| Field | Proposal C in this exercise | Proposal D in this exercise |
|---|---|---|
| Intended empty-part quantity | 500 assumed parts | 500 assumed parts |
| Parts per stack | 50 assumed | 50 assumed |
| Height of that stack | 24 cm assumed | 31 cm assumed |
| Stacks for the stated quantity | 10 calculated | 10 calculated |
| Stacks per carton and carton size | Unknown; obtain delivered arrangement | Unknown; obtain delivered arrangement |
| Arrival wrapping or compression | Not described | Not described |
| Ordinary single-part pick | Not observed | Not observed |
| Double pickup, sticking or edge damage | Not observed | Not observed |
C’s assumed stack is 7 cm shorter for the same 50 parts. That is the full supported comparison. Ten stacks do not mean ten delivery cartons, and stack height alone cannot calculate shipping volume or warehouse capacity.
Let the observed problem change the shortlist
If C fits the available storage position but repeatedly needs a second action to release one part, retain it as a proposal needing a separation response. If D separates through the intended action but its supplied stack exceeds the usable position, ask about another delivery arrangement. Neither observation makes the other proposal automatically acceptable.
A changed stack count, packing method or separation feature can answer different problems. Identify which one is proposed. A smaller stack may solve access without changing the insert; a revised formed feature may affect the insert itself. The latter needs review of any affected fit, contact or seating relationship.
Keep observed difficulty separate from its cause. Record a stuck pair or damaged location plainly before asking the supplier to assess it. No universal separation force, acceptable double-pick rate or packing speed is supplied here.
If both candidates meet the intended storage and picking requirements, compare their actual commercial offers on the same delivered scope. Include any proposed separators, wrapping and smaller bundle arrangement. Those additions can change what is supplied. The absence of a problem in a short demonstration still provides no operating-time estimate for an entire season.
Request the delivered arrangement alongside the insert
Send the component reference, intended packing action, stack-count and height record, carton questions and any located separation observation together. Ask for the proposed response against that same part and delivered state. This gives the supplier a concrete choice to address, rather than a general request for easier packing.
The delivery-state comparison guide helps distinguish supplied parts from work done after receipt. Here, make empty-stack separation an explicit part of that handover discussion.
Packrivo coordinates sourcing questions with independent suppliers. Discuss the proposed insert and its delivery stacks with Packrivo, including the candle configuration and the observation still to resolve. Actual materials, samples, quantities, pricing and timing require project-specific confirmation.
Sources and scope
- MFT-CKF manufacturing overview, undated.
- Wynalda Packaging design considerations, June 30, 2026.
- PiP Automation tray denesters, undated.
Sources checked October 26, 2026 (America/Los_Angeles). Manufacturer statements apply within their own scope. The comparison and planning images are hypothetical; no supplier delivery, sample result, operating time or transport performance has been verified.